Engineers often read ASTM A179 and A214 as two positions on one strength ladder and then argue about which is stronger. Both are carbon steel tube specifications written for heat transfer equipment, and both are governed by the same general-requirements standard, ASTM A450/A450M. What actually changes between them is the wall: A179 is seamless and cold-drawn, A214 is electric-resistance-welded from strip. That difference decides pressure capability, where the tube will corrode or fail first, what tests are run, and what the tube costs. Getting the choice wrong is expensive in exactly the direction you did not plan for.
Both are carbon steel tube specifications for heat exchangers, condensers and similar heat-transfer apparatus. Both are adopted by ASME as SA179 and SA214, so the ASTM and ASME designations describe the same requirements for each construction. Both draw their general requirements — ordering, tolerances, marking, certification and test methods — from ASTM A450/A450M, and both are ordered by outside diameter and minimum wall thickness rather than by inside diameter.
On the numbers that procurement teams check first, the two constructions sit in the same low-carbon family:
The applicable edition of ASTM A179/A179M and A214/A214M is defined by the purchase order. Values above are specification limits; actual chemistry and test results are confirmed on the Material Test Certificate.
The two standards describe two manufacturing routes, and every other difference follows from that.
A179 covers seamless cold-drawn low-carbon steel tubes. A billet is pierced and hot-rolled into a hollow shell, which is then pickled, lubricated and cold-drawn over a mandrel to the finished size. Because the tube is drawn from solid steel, there is no longitudinal weld and no joint anywhere in the wall. Cold drawing refines the surface, tightens the dimensional tolerance and produces the smooth bore that heat transfer depends on. After the final cold-draw pass the tube is heat treated at 1200 °F (650 °C) or higher to relieve drawing stress and restore ductility.
A214 covers electric-resistance-welded carbon steel tubes. Carbon steel strip is fed through forming rolls into a cylinder; a high-frequency current heats the strip edges to a molten state and the edges are pressed together to form a longitudinal weld, after which the tube is sized and tested. Welded tubes must be heat treated at 1650 °F (900 °C) or higher and cooled in air or in a controlled-atmosphere chamber; if the tube is then cold-drawn for closer tolerance or a smoother bore, it is heat treated again at 1200 °F (650 °C) or higher after the final pass. The weld is not cosmetic — it is the tube's defining feature, and it is the reason A214 is inspected differently from A179.
A214 is the welded specification. A request for "A179 welded" is a contradiction in terms, and a quotation that offers a welded tube against A179 should be questioned.
| Item | ASTM A179 / ASME SA179 | ASTM A214 / ASME SA214 |
|---|---|---|
| Full specification title | Seamless Cold-Drawn Low-Carbon Steel Heat-Exchanger and Condenser Tubes | Electric-Resistance-Welded Carbon Steel Heat-Exchanger and Condenser Tubes |
| Construction | Seamless, cold drawn | Electric-resistance-welded (ERW) from strip |
| Longitudinal weld | None | One; each tube marked "ERW" |
| General requirements | ASTM A450/A450M | ASTM A450/A450M |
| Carbon (C) | 0.06–0.18 % | 0.18 % max |
| Manganese (Mn) | 0.27–0.63 % | 0.27–0.63 % |
| Phosphorus / Sulfur | ≤ 0.035 % each | ≤ 0.035 % each |
| Min tensile strength | 325 MPa (47 ksi) | No mandatory tensile test; 325 MPa quoted from A179 |
| Min yield strength | 180 MPa (26 ksi) | No mandatory tensile test; 180 MPa quoted from A179 |
| Min elongation | 35 % (30 % above 2 in OD) | 35 % quoted for comparison |
| Max hardness | 72 HRB | 72 HRB |
| Outside diameter range | 1/8–3 in (3.2–76.2 mm) | Up to 3 in (76.2 mm) |
| Heat treatment | After final cold draw at ≥ 650 °C (1200 °F) | After welding at ≥ 900 °C (1650 °F); cold-drawn after final pass at ≥ 650 °C |
| Forming / weld tests | Flattening; flaring (or flange) | Flattening; flange; reverse flattening |
| Relative cost | Higher | Commonly 20–40 % lower |
| Typical applications | High-pressure, high-temperature, corrosive or weld-sensitive exchangers and condensers | Moderate-pressure heat exchangers, air coolers and condensers where welded tube is permitted |
Values are indicative and must be verified against the applicable ASTM/ASME edition, size and purchase order. The applicable edition is defined by the purchase order.
The chemistry looks almost identical, and in practice it is. The one structural difference is that A179 sets both a floor and a ceiling on carbon, while A214 sets only a ceiling.
| Element, % | ASTM A179 | ASTM A214 |
|---|---|---|
| Carbon (C) | 0.06–0.18 | 0.18 max |
| Manganese (Mn) | 0.27–0.63 | 0.27–0.63 |
| Phosphorus (P) | 0.035 max | 0.035 max |
| Sulfur (S) | 0.035 max | 0.035 max |
Neither specification permits the deliberate addition of alloying elements such as chromium or molybdenum to raise strength. A179's carbon floor keeps the tube soft and ductile so it can be rolled into a tubesheet and bent into U shapes without cracking; A214 accepts any carbon up to 0.18 %, since the welded strip must first be formable and weldable and the finished tube is heat treated for uniformity.
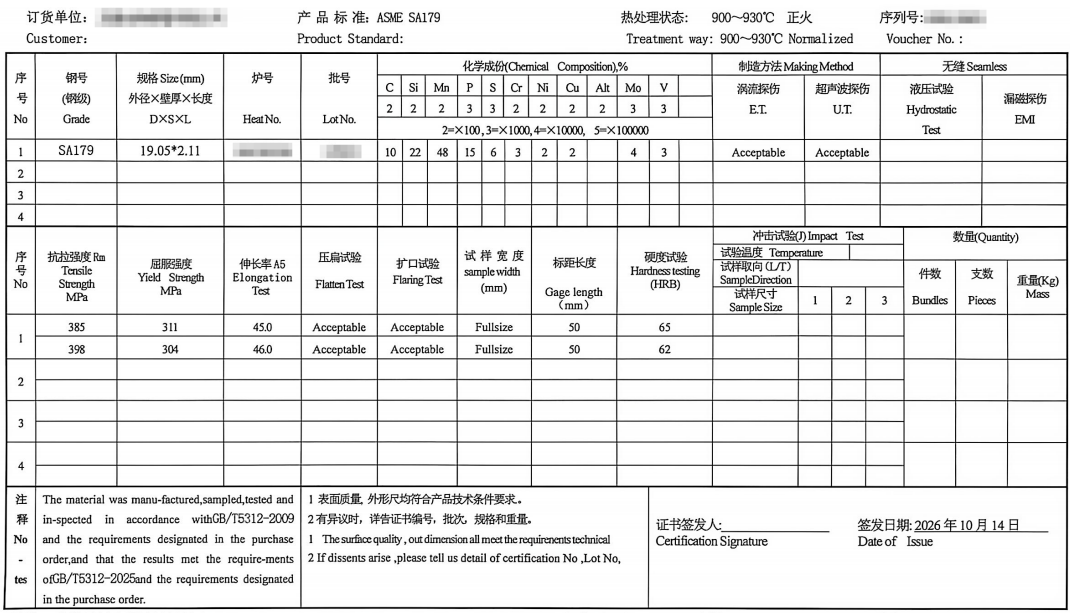
This is where the two standards stop looking alike. A179 states minimum tensile, yield and elongation values. A214 does not require a tensile test at all — its binding mechanical requirement is the hardness ceiling, checked alongside the forming and weld tests.
| Property | ASTM A179 (mandatory) | ASTM A214 |
|---|---|---|
| Tensile strength | ≥ 325 MPa (47 ksi) | No mandatory requirement; 325 MPa quoted from A179 |
| Yield strength | ≥ 180 MPa (26 ksi) | No mandatory requirement; 180 MPa quoted from A179 |
| Elongation | ≥ 35 % in 50 mm (30 % above 2 in OD) | 35 % quoted for comparison |
| Hardness | ≤ 72 HRB | ≤ 72 HRB (mandatory) |
Mechanical property requirements do not apply to tubing smaller than 1/8 in (3.2 mm) inside diameter or 0.015 in (0.4 mm) in thickness under either specification. Confirm requirements against the ordered edition and the Material Test Certificate.
The longitudinal weld is the reason a welded tube and a seamless tube are not interchangeable in pressure design. Within the ASME pressure-code framework, a seamless tube carries a joint efficiency of 1.00, while an ERW welded tube is commonly taken at 0.85. The lower factor derates the allowable stress, so for the same pressure and temperature the welded tube needs a thicker wall — in round terms about 18 % more — which narrows the apparent price advantage of the welded product.
| Factor | Seamless (A179) | Welded ERW (A214) |
|---|---|---|
| Longitudinal joint | None | One ERW seam |
| Joint efficiency (ASME framework) | 1.00 | 0.85 (typical for ERW) |
| Effect on pressure design | Baseline wall | Higher wall for the same duty |
| Corrosion / fatigue weak point | None at a seam | Weld seam and heat-affected zone if not properly annealed |
Joint-efficiency values are the ASME pressure-code framework; the governing factor is set by the design code that applies to the exchanger — for example ASME BPVC Section VIII Division 1 for shell-and-tube equipment, Section I for boilers, together with the purchase specification and any end-user requirements. Confirm the factor and the required wall against that code, not against this table.
The seam is also the first place attack begins. The weld and its heat-affected zone carry residual stress and can be anodic to the bulk metal, so in corrosive or erosive service the seam is the weak point unless it is properly annealed. That is why high-pressure, high-temperature, cyclic or aggressive duty usually resolves to seamless A179 even when welded tube would pass the pressure calculation.
Both specifications share the flattening and hardness tests, but the welded tube adds a weld-specific test and drops the flaring test that suits a seamless wall.
| Test | ASTM A179 | ASTM A214 |
|---|---|---|
| Flattening | Required (ductility) | Required (ductility and soundness; no delamination) |
| Flaring | Required, or flange test when wall < 10 % of OD | Not applicable |
| Reverse flattening | Not applicable | Required; one test per 1500 ft (450 m) of finished tube |
| Hardness | Required; ≤ 72 HRB | Required; ≤ 72 HRB |
| Hydrostatic or non-destructive electric | Each tube; purchaser specifies which | Each tube; purchaser specifies which |
The reverse flattening test splits the tube longitudinally on both sides of the weld and opens it flat, so the weld is inspected directly — it is the welded-tube equivalent of proving the seam. Eddy-current or ultrasonic testing is available on either construction where the buyer specifies it, and every A214 tube is marked "ERW" for traceability.
Both are carbon steel tube specifications for heat exchangers and condensers, and both take their general requirements from ASTM A450/A450M. The difference is the manufacturing route. A179 covers seamless cold-drawn low-carbon steel tubes, with no joint in the wall. A214 covers electric-resistance-welded, or ERW, carbon steel tubes formed from strip with a longitudinal weld. That single difference drives pressure capability, weld-seam risk, available sizes and cost.
A214 is welded. It is the electric-resistance-welded carbon steel specification for heat-exchanger and condenser tubes, and each tube is marked ERW. Its seamless counterparts are A179, A192 and A210. A quotation or order for A179 welded tube is a specification error, because A179 is defined as seamless.
Not in the same way. A179 sets mandatory minimums of 325 MPa (47 ksi) tensile and 180 MPa (26 ksi) yield. A214 does not include a tensile test among its required mechanical tests, so the 325 MPa and 180 MPa figures often quoted for A214 are comparison values taken from A179, which shares the same application. A214's binding mechanical requirement is a hardness ceiling of 72 HRB, together with the flattening, flange and reverse flattening tests.
Neither is stronger by specification. A179 sets 325 MPa minimum tensile and 180 MPa minimum yield; A214 sets no mandatory tensile minimums and in practice meets the same level, because both are low-carbon steel in the same chemistry family. The meaningful difference is construction, not strength: A179 has a continuous seamless wall, while A214 has a longitudinal weld that governs its pressure design and inspection.
Only if the specification, design code and end user permit welded tube. A214 contains a longitudinal weld, so using it where seamless tube is specified is a deviation that must be agreed with the designer. Where the service is high pressure, high temperature, cyclic or corrosive, where the weld seam is sensitive, or where the purchase specification states seamless only, A179 is required.
Yes. Seamless cold-drawn tube costs more than ERW welded tube, commonly about 20 to 40 percent more, because piercing and cold drawing are more involved than forming and welding strip. The gap narrows when the pressure design forces a thicker wall on the welded tube. Confirm current pricing against the ordered size, wall, construction and testing.
Both specifications are normally furnished up to 3 in (76.2 mm) in outside diameter, and A179 covers 1/8 in to 3 in (3.2 mm to 76.2 mm). Tubes are ordered by outside diameter and minimum wall thickness, not by inside diameter. Larger or non-standard sizes may be furnished by agreement, provided the tubes comply with the other requirements of the specification. Both can be supplied as straight lengths or as U-bend tubes.
Provide the standard and grade, ASTM A179 or ASME SA179, or ASTM A214 or ASME SA214; the outside diameter and minimum wall thickness; length and quantity; and whether straight or U-bend tubes are required. State the heat-treatment condition, end preparation, and testing — hydrostatic or non-destructive electric, with eddy-current testing where fouling or tight conditions demand it. Also state the applicable standard edition, the governing design code, and the inspection and certification scope, such as EN 10204 3.1.


.jpg)