CK45 honed tube is a cold-drawn seamless cylinder barrel made from medium-carbon CK45 steel — the European grade C45E, material number 1.1191, and the US grade SAE 1045. The bore is honed to ID tolerance H8–H9 with a mirror finish of Ra ≤0.4 µm (Ra ≤0.2 µm by skiving and roller burnishing), so the tube arrives ready to machine and assemble as a hydraulic or pneumatic cylinder barrel.
The one number that decides your wall thickness is the yield you design to: for an as-delivered CK45 barrel that is the normalized value of 340–355 MPa, not 450 MPa — 450 MPa is E355 in the +SR condition, a different steel. Three decisions settle a CK45 order: the delivery condition, whether CK45 or ST52.3/E355 is the right barrel steel, and the wall thickness the bore actually needs.
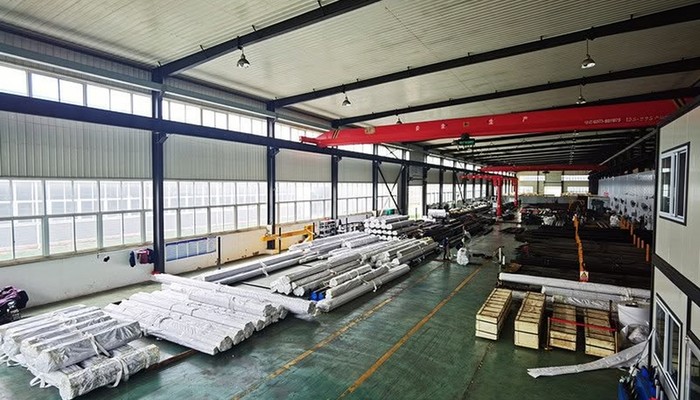
GNEE supplies CK45 honed tubes across outer diameters of 30–400 mm (1.18–15.75 in) and lengths up to 12 m (39 ft), with EN 10204 3.1 material certificates and third-party inspection on request. Send your OD × ID, wall, length and certificate requirement for a quotation.
| Parameter | Capability |
|---|---|
| Grade / material number | CK45 / C45E / 1.1191 (SAE 1045, JIS S45C) |
| Standards | DIN 2391 (St 45, withdrawn → EN 10305-1 C45E); EN 10305-1:2016; EN 10083-2; ASTM A519 (1045); JIS G3445 (STKM13C); GB/T 8713 |
| Outer diameter | 30–400 mm (1.18–15.75 in) |
| Inner diameter | 20–350 mm (0.79–13.78 in) |
| Wall thickness | To order; typical 3–40 mm (0.12–1.57 in) |
| Length | Up to 12 m (39 ft); longer by agreement |
| ID tolerance | H8–H9 (H10 available) |
| Bore roughness | Ra ≤0.4 µm (Ra ≤0.2 µm by SRB) |
| Straightness | ≤0.5 mm/m (0.5 mm per 1000 mm) |
| Delivery condition | +N (normalized), +N+SR (normalized + stress relieved), +QT (quenched and tempered) |
| Ends & preservation | Plain, bevelled or capped; rust-proof oil, plastic film, woven bag, wooden case or steel pallet |
| Certification | EN 10204 3.1; third-party inspection available |
| Element | C45E, EN 10083-2 / DIN 17200 (max) | C45E, EN 10305-1 / EN 10297-1 (max, E-grade) |
|---|---|---|
| Carbon (C) | 0.42–0.50% | 0.42–0.50% |
| Silicon (Si) | 0.40% | 0.40% |
| Manganese (Mn) | 0.80% | 0.80% |
| Phosphorus (P) | 0.045% | 0.030% |
| Sulfur (S) | 0.045% | 0.035% |
| Cr + Mo + Ni | 0.63% | 0.63% |
The E-grade versions in EN 10305-1 and EN 10297-1 tighten phosphorus and sulfur for batch consistency. Carbon at 0.42–0.50% is what makes CK45 a heat-treatable steel — and what forces preheat when the barrel is welded.
| Property | C45E, normalized (+N) | C45E, quenched & tempered (+QT, typical) |
|---|---|---|
| Yield strength Rp0.2 | ≥340 MPa (≤16 mm wall); ≥305 MPa (>16–40 mm) | ≥490 MPa (≤16 mm); ≥430 MPa (>16–40 mm) |
| Tensile strength Rm | ≥620 MPa (≤16 mm); ≥580 MPa (>16 mm) | 700–850 MPa (≤16 mm) |
| Elongation A | ≥14% (≤16 mm); ≥16% (>16 mm) | ≥14% (≤16 mm); ≥16% (>16 mm) |
| Hardness (Brinell) | 170–210 HB | 210–250 HB (mill typical) |
| Test standard | EN 10083-2 / EN 10305-1 | EN 10083-2 |
These are condition-dependent. EN 10305-1 also lists cold-drawn-hard (+C) at Rm ≥720 MPa but elongation ≥4% — too brittle for a pressure barrel; quote the condition, never just the tensile.
| Grade | Yield (as-delivered) | Carbon | Weldability | Typical barrel use |
|---|---|---|---|---|
| CK45 / C45E (1.1191) | 340–355 MPa (norm.); 490–630 MPa (+QT) | 0.42–0.50% | Poor — preheat required | Cost/availability barrels; Q+T upgrades; bolted designs |
| ST52.3 / E355 (1.0580) | ≥450 MPa (+SR) | ≤0.22% | Excellent | Welded high-pressure barrels (default) |
| 42CrMo4 (1.7225) | ≥850 MPa (+QT) | 0.38–0.45% + Cr, Mo | Moderate | Very high-strength barrels / rods |
| Condition | When to specify | Trade-off |
|---|---|---|
| Normalized (+N) or +N+SR | Routine welded or bolted barrels at moderate pressure | Lowest cost; yield 340–355 MPa; still needs preheat to weld |
| Quenched & tempered (+QT) | Higher pressure or thinner wall within the carbon-steel envelope | Yield 490–630 MPa; higher cost; poorer weldability |
| Cold-drawn hard (+C) | Structural, non-pressure parts only | Rm ≥720 MPa but A ≥4% — too brittle for a barrel |
A CK45 honed tube is a cold-drawn seamless steel tube in medium-carbon CK45 (European designation C45E, material number 1.1191, US grade SAE 1045) whose inner bore is honed to a tight ID tolerance, typically H8–H9, with a mirror-like surface roughness Ra ≤0.2–0.4 µm. It is supplied as a finished hydraulic or pneumatic cylinder barrel, ready to machine and assemble without re-boring.
Yes. They are the same steel under different naming systems: CK45 is the legacy German DIN name, C45E is the current European EN 10083-2 / EN 10305-1 designation, and SAE 1045 (AISI 1045) is the US grade. All carry material number 1.1191 and the same 0.42–0.50% carbon analysis.
For the as-delivered barrel, design to the normalized value: yield Rp0.2 ≥340 MPa at walls up to 16 mm and ≥305 MPa for thicker walls (EN 10083-2 / EN 10305-1). In the quenched-and-tempered condition yield rises to 490–630 MPa. Do not use 450 MPa — that figure belongs to E355 in the +SR condition, not CK45.
Choose ST52.3 / E355 (+SR, yield ≥450 MPa) for welded high-pressure barrels: it is stronger in the as-delivered state and welds cleanly with low carbon equivalent. Choose CK45 when cost or availability drives the spec, when the design calls for quenched-and-tempered strength, or when the cylinder is bolted rather than welded. Weldability is the deciding factor — CK45 at 0.45% carbon needs preheat and post-weld heat treatment.
Yes, but not like a low-carbon steel. With about 0.45% carbon, CK45 has a carbon equivalent CE_IIW of roughly 0.56, so welding a CK45 barrel to a flange or end cap normally requires preheating to 150–250 °C and stress-relief (post-weld heat treatment) to avoid hardening and cracking in the heat-affected zone. E355 is the safer choice where the barrel must be welded.
They are two different finished products. The honed tube is the cylinder barrel, finished on the inside bore (Ra ≤0.4 µm, no hard surface). The piston rod is induction-hardened and chrome-plated on the outside, reaching a surface hardness of 850–1150 HV. Do not copy rod hardness or strength figures onto the tube — the barrel is a through-thickness, as-delivered steel tube, not a surface-hardened component.
Typical supply range: outer diameter 30–400 mm (1.18–15.75 in), inner diameter 20–350 mm (0.79–13.78 in), length up to 12 m (39 ft) and longer by agreement, ID tolerance H8–H9 (H10 available), bore roughness Ra ≤0.4 µm (Ra ≤0.2 µm by SRB), straightness ≤0.5 mm/m. Wall thickness is supplied to order, typical 3–40 mm.
Specify EN 10305-1 as C45E (current European precision-tube standard, where C45E is a valid grade) or ASTM A519 as grade 1045. Legacy drawings reading "DIN 2391 St 45" or "DIN 17200 CK45" reference withdrawn standards; accept EN 10305-1 C45E and EN 10083-2 C45E respectively as equivalent, and confirm the edition on the order.